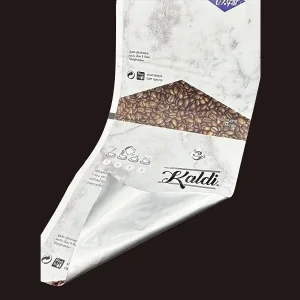
In the modern coffee industry, packaging is no longer just a vessel; it is a critical component of E-E-A-T (Experience, Expertise, Authoritativeness, Trustworthiness). As a premier wholesale manufacturer, we recognize that coffee preservation technology must balance oxygen barrier integrity with environmental stewardship.
The shift toward circular economy models has forced manufacturers to move beyond traditional multi-layer plastics. Our R&D team focuses on mono-material laminates that maintain high barrier performance for volatile organic compounds in coffee, ensuring the 'fresh-roasted' profile is preserved for longer shelf life.
We are actively transitioning toward bio-based high-barrier films. By utilizing advanced coating technologies, we achieve superior moisture resistance without compromising the recyclability of the pouch. Our GMP-certified facility ensures that every batch meets rigorous international standards for food contact safety.
We utilize recyclable mono-materials and reduction-focused manufacturing processes to minimize carbon footprints.
Yes, we provide end-to-end design, plate-making, and high-fidelity printing services tailored to your brand.
With our 35 years of manufacturing experience, we optimize production flows to ensure rapid turnaround times for global shipping.
 DongFa Printing